Non Rising Stem Gate Valve Solutions for Water Treatment
Why Non-Rising Stem Gate Valves Matter in Water Treatment
Water treatment facilities operate in demanding environments where space constraints, media consistency, and long-term operational reliability are non-negotiable priorities. Among the many valve types deployed in these systems, the non-rising stem gate valve has emerged as a preferred choice for engineers and procurement specialists managing water treatment pipelines.
Unlike rising stem configurations, non-rising stem gate valves keep the stem stationary in terms of vertical travel — the stem rotates in place while the gate travels axially within the valve body. This compact design eliminates the need for additional overhead clearance, making it particularly well-suited for underground installations, confined valve pits, and municipal water infrastructure where space is at a premium.
How Non-Rising Stem Gate Valves Function
The operational principle of a non-rising stem gate valve centers on a threaded stem that rotates within a fixed packing zone while the gate moves axially to open or close the flow path. As the handwheel or actuator turns the stem, the gate descends into the seating area, creating a positive shutoff of fluid flow. When the gate is fully retracted, the valve offers a full-bore, unobstructed passage — a critical requirement in water treatment systems where flow efficiency and pressure consistency directly affect downstream process performance.
Because the stem does not extend outward during operation, non-rising stem gate valves reduce the risk of mechanical damage to the stem in environments with limited clearance. This design also simplifies the valve pit dimensions required in municipal water distribution and treatment layouts, lowering civil engineering costs and facilitating maintenance access.
Key Challenges in Water Treatment Valve Applications
Water treatment pipelines present several chronic challenges for valve manufacturers and end users alike:
- Media contamination and particulate wear: Treated and partially treated water can carry suspended solids that accelerate seat and seal wear over time.
- Corrosion under sustained exposure: Prolonged contact with chemically treated water, chlorinated effluents, or aggressive groundwater sources can degrade valve bodies and internals.
- Seal reliability: Leakage at the stem packing or gate seat represents both a maintenance burden and a potential contamination risk in potable water and wastewater systems.
- Space and installation constraints: Many municipal and industrial water treatment installations place valves in underground chambers or compact manifold systems, limiting available clearance for rising stem mechanisms.
- Long-term lifecycle cost: Unplanned valve replacement drives up operational expenditures, making durability and consistent sealing performance a priority for facility operators.
Addressing these challenges requires gate valves engineered with material integrity, precision seating, and dimensional consistency — qualities that leading manufacturers work to embed into every stage of the production process.
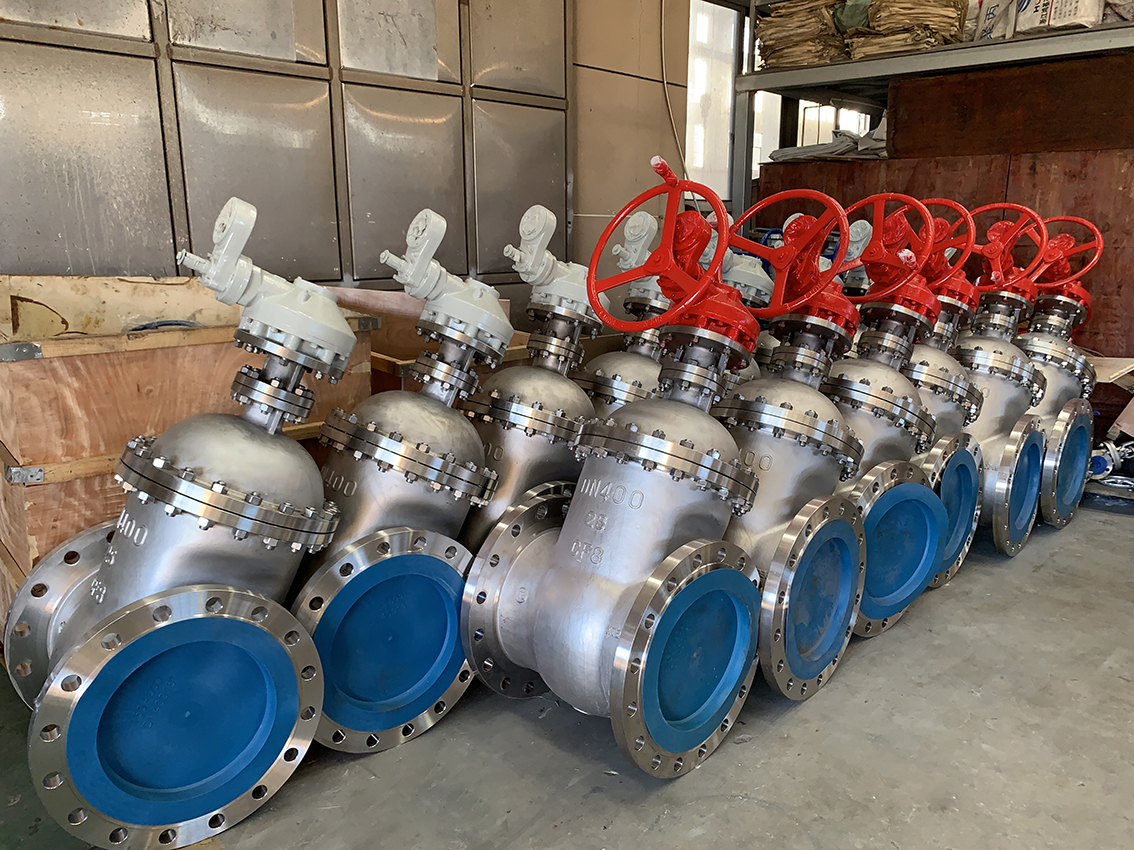
XINTAI Valve's Gate Valve Offering for Water Treatment
XINTAI Valve (XINTAI Valve Group Co., Ltd.), established in 1998 and headquartered in Wenzhou, China, manufactures a comprehensive gate valve product line that includes non-rising stem configurations specifically suited for water treatment applications. The company's gate valve range encompasses wedge, slab, pressure seal, cast steel, forged, rising stem, non-rising stem, and knife gate variants.
Within the water treatment sector, the non-rising stem design addresses the space and reliability requirements commonly encountered in municipal infrastructure, industrial water systems, and wastewater treatment facilities. XINTAI Valve's gate valve designs deliver reliable full-bore isolation performance in environments where consistent shutoff and long service intervals are essential operational requirements.
Integrated Manufacturing as a Quality Foundation
One of XINTAI Valve's defining characteristics is its integrated supply chain, which gives the company direct control over casting foundries and machining bases. This internal ownership model enables full-process quality monitoring from raw material sourcing through finished valve inspection — a significant advantage when dimensional precision and material consistency are central to valve performance in water treatment environments.
The company operates across 6 production bases located in Wenzhou, Tianjin, and Lishui, covering a total facility area of 58,800 m². With an annual production capacity of 270,000 valves, XINTAI Valve supports large-scale project supply without compromising delivery timelines.
Smart manufacturing further reinforces production consistency. XINTAI Valve deploys 13 six-axis robots for polishing and inspection tasks, delivering a 40% improvement in manufacturing efficiency while reducing production variation. For buyers procuring non-rising stem gate valves in volume, this automation infrastructure translates directly into dimensional repeatability and tighter manufacturing tolerances across production batches.
Technical Certifications Supporting Water Treatment Projects
XINTAI Valve holds a broad portfolio of internationally recognized certifications relevant to water treatment and industrial valve applications:
- ISO 9001 — quality management system certification
- ISO 14001 — environmental management system certification
- ISO 45001 — occupational health and safety management certification
- CE Certification and EU Declaration of Conformity
- API 600 and API 602 — gate valve standards for industrial applications
- API 6D — pipeline valve specification
- SIL — safety integrity level certification
These certifications confirm that XINTAI Valve's manufacturing processes, testing protocols, and product designs meet internationally accepted performance benchmarks — a prerequisite for qualification on water treatment infrastructure projects operated by engineering companies, municipal authorities, and industrial end users.
Engineering Depth and In-House Testing
XINTAI Valve maintains a dedicated in-house testing facility located in Yongjia, where pressure testing, seal validation, and material verification are conducted to confirm valve performance prior to shipment. With a technical team comprising 33 engineers, 41 testers, and 25 quality managers across a total workforce of 580 employees, the company provides the engineering depth required to support specification-driven procurement on complex water treatment projects.
For installations that involve custom engineering requirements — such as non-standard face-to-face dimensions, specialized coating systems for corrosive media, or actuator integration for automated pipeline control — XINTAI Valve's custom valve engineering capability allows tailored solutions to be developed in compliance with applicable standards.
Market Reach and Supplier Credibility
XINTAI Valve's global footprint spans North America, South America, Europe, Central Asia, the Middle East, and Southeast Asia. The company holds certified supplier designations from Petronas and Petrobras, reflecting its capacity to meet the rigorous qualification requirements imposed by major energy and industrial operators. The underlying supply chain discipline, quality management infrastructure, and project execution capabilities that earned these designations translate directly to the demands placed on valve suppliers in water treatment markets, where project consistency, documentation completeness, and traceability are equally important.
Summary
The non-rising stem gate valve occupies a specific and valuable position in the water treatment valve landscape, offering space-efficient installation, reliable shutoff performance, and full-bore flow capacity when open. For procurement professionals, plant engineers, and project managers evaluating gate valve supply for water treatment applications, XINTAI Valve Group Co., Ltd. presents a manufacturing profile built on integrated production control, automation-driven consistency, international certification compliance, and over two decades of industrial valve experience — making it a credible and capable source for non-rising stem gate valve requirements across a broad range of water treatment project scales.
www.xintaivalves.com
Xintai Valve Group Co., Ltd.
