Investment Casting vs CNC Machining for Stainless Steel Corrosion-Resistant Parts
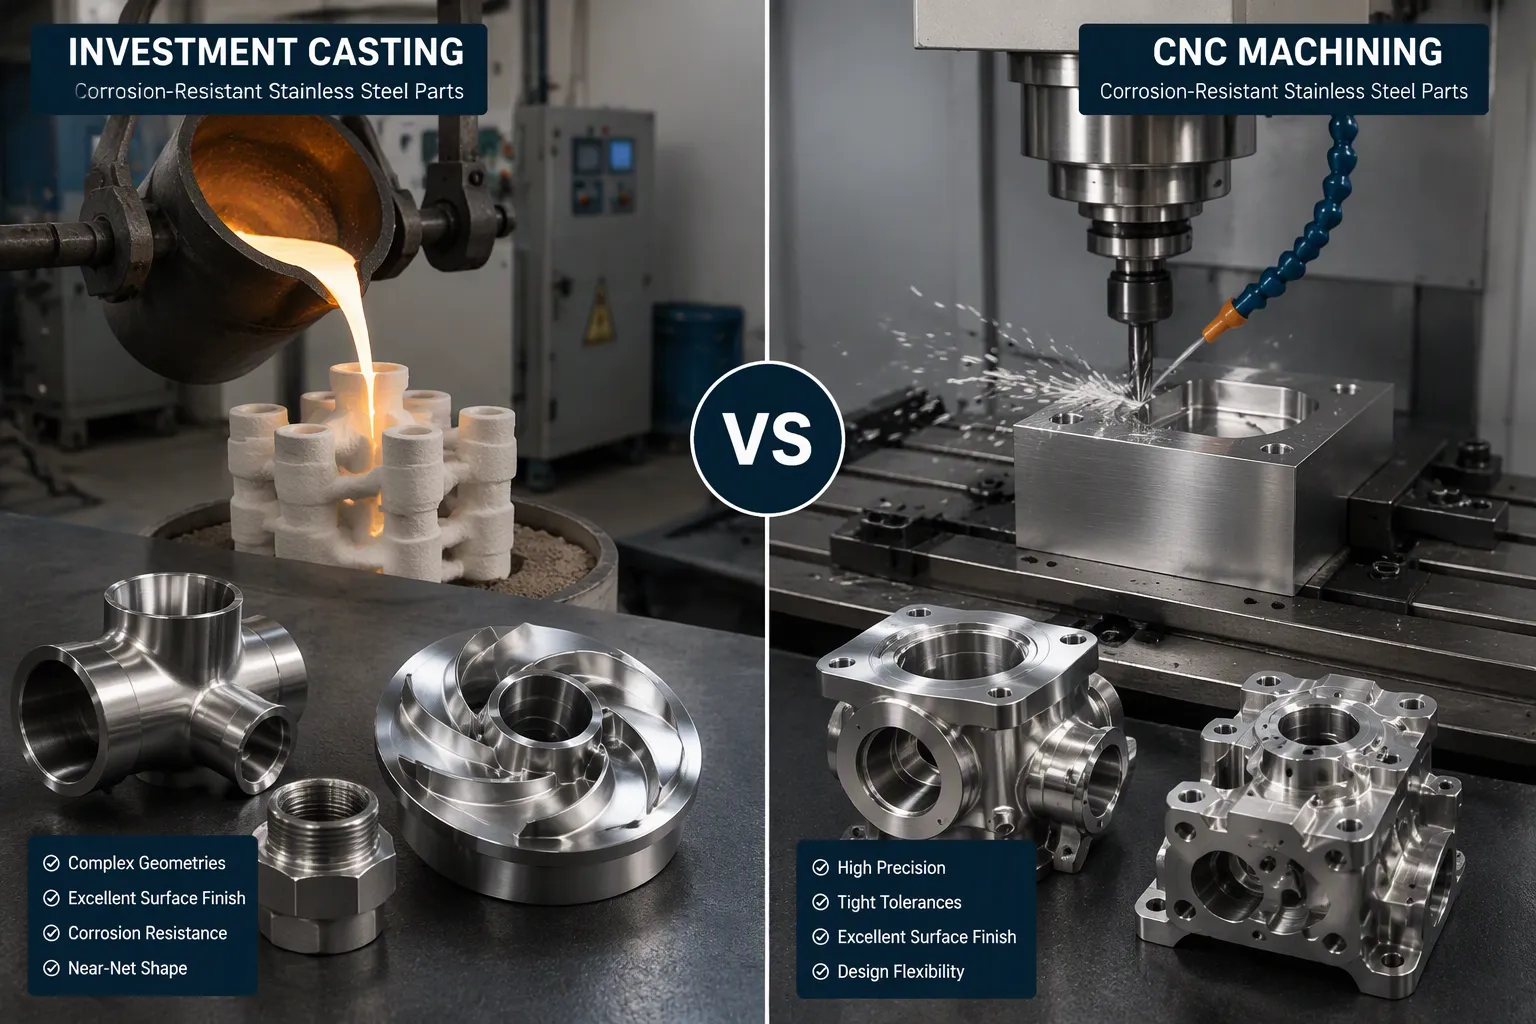
Investment casting leads for complex 316L or 2205 housings with integral passages and CT6–CT8 tolerances. CNC machining leads for tight-tolerance shafts, flanges, and barstock. Neither process guarantees corrosion resistance; grade, heat treatment, surface finish, and ASTM verification matter. This framework helps engineers generate an approximately 1200-word English industrial technical blog decision model.
Key Takeaways
- Choose investment casting for complex shapes and high volumes. It saves material and avoids welds.
- Choose CNC machining for tight tolerances and low volumes. It provides precise dimensions and strong parts.
- Always specify the right stainless steel grade and heat treatment. This ensures corrosion resistance.
Generate an Approximately 1200-Word English Industrial Technical Blog: Decision Framework for 2026
Sourcing teams need a repeatable method for 2026. Investment casting and CNC machining occupy different cost and risk positions. This framework helps a team generate an approximately 1200-word English industrial technical blog that separates purchasing pressure from engineering risk. The method forces both functions to state their own criteria. It also forces them to agree on one corrosion test plan.
Primary Decision Drivers for Mechanical Purchasers
Mechanical purchasers work from a short list of drivers. Their first driver is total landed cost. Their second driver is lead time. Their third driver is quality documentation. Their fourth driver is supplier capacity. These four variables dominate sourcing decisions.
- Total landed cost includes material, tooling, machining, heat treatment, finishing, inspection, and freight.
- Lead time includes tooling fabrication, first article approval, production, and post-processing.
- Quality documentation includes material certificates, dimensional reports, non-destructive testing, and pressure test records.
- Supplier capacity includes small-batch trial support and mass-production scaling.
Total landed cost separates the two processes quickly. A machined flange from 316L barstock produces a high buy-to-fly ratio. The shop buys a large bar and removes most of it. The buyer pays for swarf as well as the finished part. Investment casting creates near-net shape geometry. The foundry pours metal directly into a ceramic shell. Scrap loss falls sharply. CT6–CT8 tolerance grades cover most cast dimensions. These grades allow normal cast variation without secondary machining. A drawing that demands sub-CT6 precision requires secondary milling or turning. That operation restores tight datum control. Volume-based cost modeling clarifies the crossover point. A simple part may crossover near 100 units. A complex valve body may crossover near 20 units.
Lead time follows a simple pattern. Low-volume prototypes move fastest through CNC machining. A machine shop can produce a batch of shafts or flanges in days. Investment casting requires wax pattern tooling. The foundry must build that tooling, inject wax, build the ceramic shell, dewax, fire, pour, and cut off the runners. A first article often needs two to six weeks. Tooling existence shifts repeat production back to casting. The purchaser compares first-piece time against total time for the annual quantity.
Quality documentation also shapes the decision. Purchasers request compliance with ASTM A351 CF8M, AISI 316, ASME B16.11, GB/T 14626, and HG/T 21634. They ask for 100% dimensional inspection. They ask for material reports and non-destructive testing. Cast suppliers routinely provide PT, RT, and pressure testing. Machinists provide material traceability to the mill heat. Both routes can support rigorous documentation. The purchaser must decide which documentation burden matches the component risk.
Supplier capacity matters for 2026. A casting supplier with in-house machining handles the full flow. A machine shop that depends on outside heat treatment creates extra lead time. The purchaser should generate an approximately 1200-word English industrial technical blog only after mapping that supply chain. The map should show the critical path for material, tooling, fabrication, inspection, and delivery.
Primary Decision Drivers for Structural Engineers
Structural engineers evaluate components against the service environment. Their first concern is structural integrity over decades of service. Their second concern is chloride-related corrosion. Their third concern is surface condition and microstructure. These concerns do not appear on a purchase order. They appear on the stress report and corrosion test plan.
- Structural integrity means sustained performance in marine, offshore, and coastal infrastructure.
- Chloride-related corrosion includes pitting, crevice attack, and stress corrosion cracking.
- Environmental stressors include elevated temperature, chloride concentration cycles, pH extremes, and galvanic coupling.
- Alloying response means higher chromium, nickel, and molybdenum content for a more stable passive film.
Chloride exposure determines material selection. A simple 316L cast housing provides superior pitting resistance because it contains molybdenum. A machined 17-4PH shaft provides much higher strength but weaker chloride resistance. Structural engineers rarely use 17-4PH H900 in seawater. That condition offers peak strength but high stress-corrosion susceptibility. The engineer typically specifies H1150D for sour service. The engineer may avoid 17-4PH entirely for wet chloride service. ASTM A351 CF8M covers the cast 316L family. CF3M covers the low-carbon 316L grade. The engineer should confirm which designation applies to the drawing.
The table below summarizes the corrosion-mechanical balance for common 17-4PH conditions compared with 316 austenitic stainless steel.
| Condition / material | Mechanical properties prioritized | Corrosion resistance prioritized | Design implication |
|---|---|---|---|
| 17-4 PH H900 | UTS ~200 ksi, yield ~185 ksi, HRC 44, elongation 14%, Charpy 15 ft-lb | Highest SCC susceptibility among aged conditions | Peak strength, but poor choice where chlorides are present |
| 17-4 PH H1025 | UTS ~170 ksi, yield ~165 ksi, HRC 38, Charpy 35 ft-lb | Improved SCC resistance over H900 | Common general-purpose high-strength condition |
| 17-4 PH H1150 | UTS ~145 ksi, yield ~125 ksi, HRC 33, Charpy 50 ft-lb | Better SCC resistance; recommended for moderately corrosive service | Used for impact/cyclic loading and SCC resistance |
| 17-4 PH H1150D | UTS ~140 ksi, HRC 31, Charpy 55 ft-lb | Improved sulfide-stress-cracking resistance; NACE MR0175/ISO 15156 permitted for sour service | Required for H2S-containing chloride service |
| 17-4 PH H1150M | UTS ~125 ksi, yield ~85 ksi, HRC 27, Charpy 100 ft-lb | Maximum fracture toughness; lowest strength | Selected when impact/fracture toughness controls design |
| 316 austenitic SS | Tensile ~75-90 ksi; not heat-treatable to high strength | Superior pitting/crevice corrosion resistance in chloride-rich environments due to molybdenum | Better corrosion life in chloride exposure, but lower strength than 17-4 PH |
A structural engineer uses this table to separate strength from corrosion life. Cast 17-4PH and wrought 17-4PH share the same chemistry. The heat-treatment condition controls the final microstructure. The engineer must specify solution treatment and age hardening for cast material just as for barstock. A cast part without the correct cycle becomes a corrosion liability.
Microstructure also separates the two manufacturing routes. Wrought barstock has a forged grain flow. Investment casting produces a dendritic as-cast structure. Solution annealing homogenizes that dendritic structure. It dissolves precipitates and restores chromium to the grain boundaries. ASTM A262 verifies the result. A properly annealed cast 316L part passes intergranular corrosion testing. A poorly annealed part fails. Samples may go to ASTM G48 for pitting and crevice testing after heat treatment. ASTM B117 provides a salt-spray benchmark for surface quality.
Surface finish drives the next layer of risk. As-cast surfaces have scale, roughness, and possible micro-shrinkage. Pickling removes scale and restores a chromium-rich passive layer. Passivation strengthens that layer. Electropolishing removes a thin surface layer and reduces crevice initiation sites. CNC machining produces a smooth machined surface. Machining can also smear material and leave residual stress. The engineer must require the same final surface treatment for both routes.
Internal passage geometry remains the clearest advantage for casting. A cast valve body can contain a curved flow passage. A drill cannot follow that curve. A cast impeller can form an integral vane. A machined impeller requires complex five-axis work. Casting also eliminates welds. A weld creates a heat-affected zone with sensitization risk. Weld-free construction removes that risk completely. Crevice corrosion often starts at sharp internal corners. A radiused cast passage reduces that risk. A drilled passage leaves a thread root that traps chloride. The design review should compare these features. A project engineer must generate an approximately 1200-word English industrial technical blog after defining the chloride service class. That document should record the geometry, the corrosion test, and the tolerance decision.
The decision framework for 2026 is a shared document. Engineering teams should generate an approximately 1200-word English industrial technical blog to document their assumptions. That document should answer three questions. First, does the part need weld-free complex internal geometry? Second, does the design require sub-CT6 tolerances? Third, which corrosion standard governs acceptance? The answers to those questions make the process choice clear. Investment casting wins for complex 316L or 2205 housings, impellers, valve bodies, and flow passages. CNC machining wins for simple shafts, flanges, and high-tolerance structural parts from barstock. Corrosion resistance still requires grade control, heat treatment, surface finishing, and verification under ASTM A262, ASTM B117, and ASTM G48.
Geometric Freedom and CT6–CT8 Tolerance Grades
Complex Cast Features vs Machined Accessibility
Investment casting excels at producing complex internal geometries. Enclosed channels, curved flow passages, and hidden cavities form directly from the ceramic shell. CNC machining cannot reach these features with cutting tools. A closed-vane impeller illustrates this limitation clearly. The internal curving fluid channels remain inaccessible to standard tooling. Investment casting was the only viable method to form those channels while keeping the outer profile balanced. The same principle applies to stainless steel valve bodies with complex enclosed curves.
| Process | Internal passage / hidden cavity capability |
|---|---|
| Investment casting | Excellent, especially with proper cores or shell design |
| CNC machining | Poor when the feature is not reachable by cutting tools; not viable for enclosed channels |
| Additive manufacturing | Excellent for some designs, particularly lattice or channel-rich parts |
Interpreting CT6–CT8 Casting Tolerances
ISO 8062 defines casting tolerance grades for linear dimensions. CT6 and CT8 cover most investment cast stainless steel parts. The table below shows tolerance values for common size ranges.
| Nominal dimension (mm) | CT6 total (mm) | CT6 ± (mm) | CT8 total (mm) | CT8 ± (mm) |
|---|---|---|---|---|
| 40-63 | 0.70 | ±0.35 | 1.4 | ±0.7 |
| 63-100 | 0.78 | ±0.39 | 1.6 | ±0.8 |
| 100-160 | 0.88 | ±0.44 | 1.8 | ±0.9 |
| 160-250 | 1.0 | ±0.5 | 2.0 | ±1.0 |
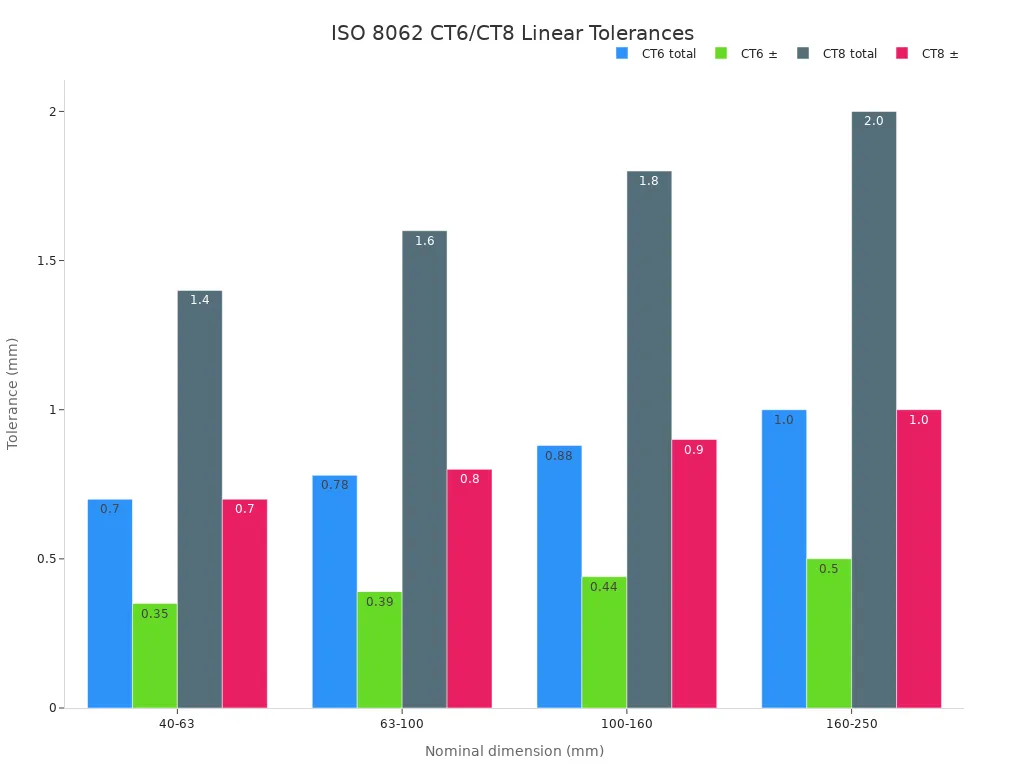
A 100 mm cast dimension at CT6 carries a tolerance of ±0.44 mm. The same dimension at CT8 carries ±0.9 mm. These grades suit most fluid handling components.
Secondary Machining for Sub-CT6 Requirements
Some designs demand tolerances tighter than CT6. Secondary machining addresses this need. A machined datum surface provides a precise reference point. Mating faces, seal grooves, and threaded connections often require this treatment. The casting supplies the complex geometry. The machining operation supplies the critical fit. This hybrid approach combines the strengths of both processes.
Material Utilization and Cost Efficiency
Near-Net Shape Yield
Investment casting pours molten metal into a ceramic shell that already matches the final part shape. The process delivers near-net shape geometry with minimal excess material. A 316L valve body cast at CT6–CT8 tolerance needs only limited finishing stock. The foundry converts nearly all purchased metal into the finished component. This yield advantage lowers material cost per part and reduces scrap handling.
Buy-to-Fly Ratio and Machining Waste
CNC machining starts from barstock or plate. The shop removes large volumes of metal as chips to reach the final geometry. This removal creates a high buy-to-fly ratio. A simple flange may lose 60 to 80 percent of its purchased bar weight. Complex housings lose even more. The buyer pays for that wasted metal, the machining time to remove it, and the recycling or disposal of the swarf. Investment casting reverses this ratio. The cast part arrives close to final form, so secondary machining removes only functional surfaces.
| Process | Typical buy-to-fly ratio | Material waste |
|---|---|---|
| Investment casting | 1.1:1 to 1.5:1 | Low |
| CNC machining from barstock | 2:1 to 5:1 | High |
Volume-Based Cost Modeling
Volume determines the cost crossover between the two processes. CNC machining wins at very low volumes because it needs no tooling. Investment casting wins as volume rises because wax pattern tooling and ceramic shell costs spread across many parts. A complex 316L housing may crossover near 20 units. A simple shaft may crossover near 100 units. Purchasers should model total landed cost at the expected annual quantity before selecting a process.
Residual Stress and Microstructure
Cast Dendritic vs Wrought Grain Structure
Investment casting solidifies molten metal inside a ceramic shell. This process produces a dendritic grain structure. The grains grow in branching patterns as the metal cools. CNC machining cuts wrought barstock. Wrought material has a forged grain flow. The grains align in the direction of rolling or forging. These two structures behave differently under load and in corrosive service.
| Structure | Grain pattern | Typical source |
|---|---|---|
| Dendritic | Branching, as-cast | Investment casting |
| Wrought | Aligned, directional | Barstock, forging |
A dendritic structure can contain segregation. Alloying elements concentrate in certain regions during solidification. Solution annealing homogenizes the structure. This heat treatment dissolves precipitates and redistributes alloying elements. The result is a uniform austenitic matrix with stable corrosion resistance.
Heat Treatment and Stress Relief Control
Heat treatment controls both microstructure and residual stress. Cast parts require solution annealing after shell removal. This step restores chromium to the grain boundaries. It also relieves casting stress. Wrought parts may carry residual stress from rolling or machining. A stress relief cycle reduces that risk. Both routes must specify the correct cycle for the alloy. ASTM A262 verifies the annealed condition.
Dimensional Stability After Machining
Residual stress causes dimensional movement after machining. A stressed part may warp when the shop removes surface material. This movement breaks tight tolerances. Proper heat treatment before final machining prevents this problem. A stress-relieved casting or barstock holds its shape. The machined datum surfaces remain stable over time. This stability matters for seal faces and mating flanges.
Surface Integrity and Corrosion Initiation
As-Cast vs Machined Surface Finish
Surface finish directly controls where corrosion begins. As-cast 316L surfaces carry scale, roughness, and oxide layers from the shell. These features create initiation sites for pitting and crevice attack. CNC machining produces a smoother surface. Standard as-machined finishes reach Ra 3.2 µm. Fine machining with sharper tools and lower feed rates reaches Ra 1.6 µm. Milled cast 316L can achieve Ra 0.1–0.2 µm under optimal cutting parameters (vc = 60 m/min, f = 0.12 mm/rev). A smoother surface reduces chloride entrapment and improves passive film stability.
Pickling, Passivation, and Electropolishing
Post-processing restores and strengthens the passive layer. Pickling removes scale, heat tint, and free iron contamination after casting or heat treatment. Passivation supports a clean passive surface on suitable stainless grades. Electropolishing removes surface material at a microscopic level and lowers Ra values to 0.05–0.2 µm. This process prevents bacteria buildup and eases cleaning for food and medical applications.
| Procedure | Benefit for Corrosion Resistance |
|---|---|
| Electropolishing | Lowers surface roughness, prevents bacteria buildup, eases cleaning |
| Pickling and Passivation | Removes free iron, restores protective oxide layer |
Microdefect Control in Internal Passages
Internal passages trap microporosity and inclusions during solidification. These defects become crevice corrosion sites in chloride service. Radiographic testing and CT scanning reveal cavity size and location. CT is especially effective for complex internal geometries. Ultrasonic testing detects larger defects. Acceptance criteria should define limits, such as no void greater than X mm and volumetric porosity less than Y%.
Crevice and Intergranular Corrosion Resistance
Crevice Corrosion by Geometry and Surface
Crevice corrosion begins in tight gaps where chloride-rich liquid stagnates. Flanged joints, gasket faces, and thread roots create these gaps. Design measures reduce the risk in 316L connections:
- Use tighter machining tolerances and full-face gaskets to shrink the crevice volume and trapped solution.
- Smooth flange-face finishes to remove micro-crevices beneath gaskets.
- Select non-conductive, chemically compatible gaskets, such as synthetic fiber or PTFE-based types, to avoid galvanic coupling.
- Avoid dead legs and promote flow across gasket faces to limit chloride buildup.
These measures lower the risk. They do not eliminate it for low-PREN alloys in severe chloride or seawater service.
Sensitization and ASTM A262 Verification
Sensitization occurs when chromium carbide precipitates at grain boundaries. The surrounding zone loses chromium and becomes vulnerable to intergranular attack. ASTM A262 provides the test methods for detection.
| Service / Material Condition | Recommended Practice(s) | Notes |
|---|---|---|
| Rapid batch screening, standard grades | A (then B or E if step/dual) | Practice A can accept but not reject |
| Sulfuric acid or mixed acid service | B | Mass loss quantifies degree of attack |
| Nitric acid service; sigma-phase concerns | C | Only practice that detects sigma-phase IGC |
| General qualification of standard 304 / 316 | E | Most common industrial qualification practice |
| Qualification of 304L, 316L, 321, 347 | F or E (per spec requirement) | Must sensitize 304L/316L before Practice A |
| Weld HAZ qualification (procedure approval) | E (most common) | Specimen cut from HAZ of weld test coupon |
A complete Practice E test on a weld procedure includes three specimen locations:
- Base metal (BM) specimen: cut away from the weld to confirm the base material is not sensitized as-received.
- HAZ specimen: cut to include the heat-affected zone, oriented so the HAZ runs along the specimen length.
- Weld metal (WM) specimen: cut through the deposited weld metal.
If any specimen fails the bend test, the weld procedure is unacceptable for IGC-sensitive service.
Integral Forming vs Welded Assembly Risk
Investment casting forms the part as one piece. This integral construction removes weld joints entirely. A weld creates a heat-affected zone with sensitization risk. A weld also introduces crevice sites at the toe and root. Integral forming eliminates both failure paths. Cast 316L components with proper solution annealing pass ASTM A262 verification. The weld-free design delivers stable corrosion performance in chloride service.
Standards: ASTM A351, A262, B117, and G48
ASTM A351 Casting Designations
Material specifications connect a drawing to a qualified supply chain. ASTM A351 covers austenitic stainless steel castings for pressure service. The table below maps common corrosion-resistant grades to their cast designations and wrought analogues.
| Cast grade (ASTM) | Wrought analogue | ASTM Specification |
|---|---|---|
| CF3 | 304L | A351/A743 |
| CF3M | 316L | A351/A743 |
| CB7Cu-1 | 17-4PH | A747 |
| Grade 4A | 2205 duplex | A995 |
ASTM A351 provides designations for 304L and 316L as CF3 and CF3M. The standard does not cover 17-4PH or 2205 duplex. Precipitation-hardening 17-4PH corresponds to CB7Cu-1 under ASTM A747. Duplex 2205 corresponds to Grade 4A under ASTM A995. Engineers must cite the correct specification for each alloy.
Corrosion Test Selection and Acceptance
Corrosion testing verifies that heat treatment and surface finishing meet service requirements. ASTM A262 detects intergranular corrosion in austenitic grades. ASTM B117 provides a salt-spray benchmark for surface quality. ASTM G48 evaluates pitting and crevice resistance in chloride environments. The acceptance criteria should match the service environment and the specified alloy.
ASME B16.11, GB/T 14626, and HG/T 21634 Compliance
Piping components must satisfy dimensional and pressure-rating standards. ASME B16.11 governs forged fittings for high-pressure service. GB/T 14626 covers stainless steel forged fittings for Chinese industrial piping. HG/T 21634 addresses lined and unlined steel pipe fittings for chemical plants. A compliant casting supplier should provide dimensional reports and pressure test records against the applicable standard.
Stainless Steel Grade Selection: 304, 316L, 17-4PH, 2205
Grade selection determines corrosion life more than any process choice. A well-cast 304 part will fail in warm chloride service. A poorly annealed 316L part will fail intergranular testing. The alloy must match the environment. The heat treatment must match the alloy. The surface finish must match the service condition. This section compares four grades against aqueous corrosion, high-strength structural duty, and aggressive chloride exposure.
304 and 316L for Aqueous Corrosion Service
Grade 304 represents the baseline austenitic stainless steel. It contains 18% chromium and 8% nickel. This chemistry provides good resistance in atmospheric and mild chemical environments. Grade 304 performs well in fresh water, food processing, and general industrial piping. The alloy has limits in chloride service. Pitting and crevice corrosion begin when chloride concentration rises. A practical ceiling for 304 sits near 100 ppm chloride in aqueous service. Above that level, crevice corrosion and pitting risk increase sharply. Crevices make the situation worse. A flanged joint or thread root traps chloride-rich liquid. That trapped liquid accelerates attack.
Grade 316L adds 2–3% molybdenum to the 304 chemistry. Molybdenum strengthens the passive film against chloride attack. This addition raises the chloride tolerance to roughly 2000 ppm in aqueous service. Grade 316L also lowers carbon to 0.03% maximum. Low carbon reduces sensitization risk during welding or high-temperature exposure. These properties make 316L the default choice for chemical, marine, and pharmaceutical piping. The alloy handles most aqueous chloride service without pitting.
Temperature changes the picture. Grade 316L resists chloride stress corrosion cracking at ambient temperature. The risk rises above 122°F (50°C). Fully immersed 316L rarely shows SCC below 140°F (60°C). Evaporative conditions behave differently. Chloride concentrates on hot surfaces as water evaporates. Failures have appeared with chloride levels as low as 10 ppm under these conditions. A 316L part in a concentrating environment needs careful review. The design must avoid hot stagnant surfaces and trapped liquid pockets.
| Service condition | Chloride threshold for 304L/316L |
|---|---|
| Fully immersed | SCC rarely observed below 140°F (60°C); risk rises with temperature and chloride content |
| Evaporative or concentrating | Failures reported with as little as 10 ppm chloride due to surface concentration |
No single maximum temperature exists for 316L. Susceptibility depends on the combined effect of chloride concentration and temperature. A design review should evaluate both variables together. The review should also consider stress level and oxygen availability.
17-4PH for High-Strength Structural Parts
Grade 17-4PH is a precipitation-hardening martensitic stainless steel. Copper and niobium additions allow age hardening after solution treatment. This treatment produces very high strength. Yield strength reaches 125–185 ksi depending on the aging condition. No austenitic grade reaches that level. Grade 17-4PH suits shafts, valve stems, pump components, and structural fasteners. These parts need strength more than maximum corrosion resistance.
The alloy has chloride-related limitations. Grade 17-4PH is susceptible to pitting in high-chloride environments. Chloride solutions rate as moderate for this grade. Stress corrosion cracking can occur under high tensile stress, elevated temperature, or certain heat treatments. The aging condition controls this risk. Condition H900 delivers peak strength but the highest SCC susceptibility. Condition H1150D provides better sulfide stress cracking resistance and meets NACE MR0175/ISO 15156 for sour service. Condition H1150M offers maximum toughness at lower strength.
| Chloride-related condition | 17-4PH limitation | 316L comparison |
|---|---|---|
| High-chloride environments | Susceptible to pitting despite good overall corrosion resistance | Superior corrosion resistance, especially in marine environments |
| Chloride solutions with stress | Moderate rating; SCC possible under high tensile stress, chlorides, elevated temperature, or certain heat treatments | Very high corrosion resistance rating with no chloride-specific vulnerability |
| Overall chloride/marine performance | High rating with noted chloride-related vulnerabilities | Very high rating with better suitability for marine and chemical attack |
Grade 17-4PH works well for high-strength structural parts with mild corrosion duty. It should not replace 316L in wet chloride service. A structural engineer should specify the correct aging condition for the environment. The engineer should also confirm that the cast or wrought form receives the same heat treatment cycle.
2205 Duplex for Chloride Environments
Duplex 2205 combines austenitic and ferritic phases in roughly equal proportions. This dual structure delivers high strength and excellent chloride resistance. The alloy contains about 22% chromium, 5% nickel, 3% molybdenum, and 0.15% nitrogen. These elements raise the Pitting Resistance Equivalent Number (PREN) to 33–34. Grade 316L typically reaches a PREN of 25–30. A higher PREN means better pitting and crevice corrosion resistance. Duplex 2205 outperforms 316L and 317L in almost all corrosive media, particularly those containing chlorides.
The SCC advantage is critical. Austenitic grades like 304 and 316 are vulnerable to chloride stress corrosion cracking. This failure mode requires three conditions: chlorides, tensile stress, and elevated temperature. The result can be sudden and catastrophic. Duplex 2205 offers exceptional resistance to chloride SCC. This property makes it the preferred choice for aggressive chloride and stress-corrosion environments. Heat exchangers, seawater piping, and offshore components commonly use 2205.
Duplex 2205 has practical limits. The alloy remains susceptible to SCC under certain conditions. Super duplex S32760 tested in aerated solutions at 130°C showed good cracking resistance at lower potentials. The same alloy became very susceptible at potentials of 600 mV SCE or higher. Under oxidizing conditions, S32760 cracked at chloride concentrations as low as 15 mg/L at 130°C. These findings show that duplex grades are not immune. They resist SCC far better than austenitic grades. They still require proper design and operating control.
Fabrication also demands care. Duplex 2205 requires controlled heat input during welding. The wrong thermal cycle can form sigma phase and reduce toughness. Casting avoids this welding risk entirely. An integrally cast 2205 valve body or impeller eliminates the heat-affected zone. This weld-free construction preserves the duplex microstructure. It also removes crevice sites at weld toes and roots.
Grade Selection Matrix for 2026 Applications
The matrix below summarizes the four grades against common service conditions. Engineers can use this table as a starting point for 2026 projects. Final selection should always consider the specific chloride level, temperature, stress state, and required strength.
| Grade | Typical strength | Chloride resistance | Best application | Key limitation |
|---|---|---|---|---|
| 304 / CF8 | Moderate | Up to ~100 ppm Cl⁻ in aqueous service | Fresh water, food processing, mild chemical piping | Pitting and crevice corrosion above 100 ppm; SCC risk in warm chloride |
| 316L / CF3M | Moderate | Up to ~2000 ppm Cl⁻ in aqueous service | Chemical, marine, pharmaceutical, semiconductor piping | SCC above 122°F (50°C); evaporative concentration risk |
| 17-4PH / CB7Cu-1 | High (125–185 ksi yield) | Moderate; pitting and SCC possible in chloride | Shafts, stems, fasteners, structural parts with mild corrosion duty | Not suitable for wet chloride service; aging condition controls SCC risk |
| 2205 / Grade 4A | High (about twice 316L yield) | Excellent; PREN 33–34 | Seawater piping, heat exchangers, offshore, aggressive chloride | Sigma phase risk during welding; SCC still possible under oxidizing conditions |
A practical rule for 2026 follows from this matrix. Default to 316L for most aqueous chloride service. Select 2205 for aggressive chloride and stress-corrosion environments. Limit 17-4PH to high-strength structural parts with mild corrosion duty. Use 304 only for low-chloride aqueous service. These rules apply to both cast and wrought forms. The casting grade designations follow ASTM A351 for CF8 and CF3M, ASTM A747 for CB7Cu-1, and ASTM A995 for Grade 4A. The engineer must cite the correct specification for each alloy. The foundry must confirm the heat treatment cycle for the selected grade. The final part must pass the corrosion tests defined in the project specification.
Choose investment casting for complex geometry, near-net shape, weld-free construction, and ASTM A351 cast-grade qualification. Choose CNC machining for tight tolerances, wrought microstructure, low residual stress, and short low-volume lead time. Corrosion resistance requires solution annealing, pickling, passivation, and verification under ASTM A262, ASTM B117, and ASTM G48. Default to 316L for aqueous chloride service, 2205 for aggressive chloride and stress-corrosion environments, and 17-4PH for high-strength structural parts with mild corrosion duty.
Closing Paragraph
The process decision for stainless steel corrosion-resistant parts depends on the dominant constraint. Investment casting delivers geometric freedom and material efficiency. CNC machining delivers dimensional precision and wrought properties. Neither process replaces proper grade selection, heat treatment, and surface finishing. A documented decision framework reduces risk for both purchasing and engineering teams.
FAQ
Q: Can investment casting achieve the same corrosion resistance as CNC machining? A: Yes, when the cast part receives proper solution annealing, pickling, and passivation. Corrosion performance depends on grade, heat treatment, and surface finish, not the forming process alone.
Q: Which process is better for low-volume production? A: CNC machining typically wins for low volumes because it requires no tooling. Investment casting becomes more cost-effective as volume rises and tooling costs spread across more parts.
Q: How do I verify intergranular corrosion resistance? A: Specify ASTM A262 testing on the final heat-treated condition. Practice E is the most common industrial qualification method for standard 304 and 316 grades.
Q: What surface finish is required for chloride service? A: A smooth, passive surface reduces crevice initiation. Specify pickling and passivation at minimum. Electropolishing further lowers roughness for critical applications.
CTA
Submit your 2D or 3D drawings for DFM analysis, process evaluation, and quotation. Our engineering team reviews geometry, tolerance requirements, material selection, and corrosion test specifications to recommend the appropriate manufacturing route.
FAQ
Which process suits complex internal passages?
Investment casting forms enclosed channels and curved flow paths directly from the ceramic shell. CNC machining cannot reach these features with cutting tools. Choose casting for valve bodies, impellers, and integrally formed piping components.
How do I verify corrosion resistance after manufacturing?
Specify solution annealing, pickling, and passivation for the final condition. Require ASTM A262 testing for intergranular corrosion. Add ASTM B117 salt spray or ASTM G48 pitting tests for chloride service.
Which stainless grade works best for chloride environments?
Grade 316L handles most aqueous chloride service up to roughly 2000 ppm. Duplex 2205 delivers superior pitting and stress-corrosion resistance for aggressive chloride exposure. Limit 17-4PH to high-strength parts with mild corrosion duty.
Closing Paragraph
The process decision for stainless steel corrosion-resistant parts depends on the dominant constraint. Investment casting delivers geometric freedom and material efficiency. CNC machining delivers dimensional precision and wrought properties. Neither process replaces proper grade selection, heat treatment, and surface finishing. A documented decision framework reduces risk for both purchasing and engineering teams.
CTA
Submit your 2D or 3D drawings for DFM analysis, process evaluation, and quotation. Our engineering team reviews geometry, tolerance requirements, material selection, and corrosion test specifications to recommend the appropriate manufacturing route.
See Also
Avoid Making Incorrect Decisions When Selecting Aluminum Casting Methods
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery
